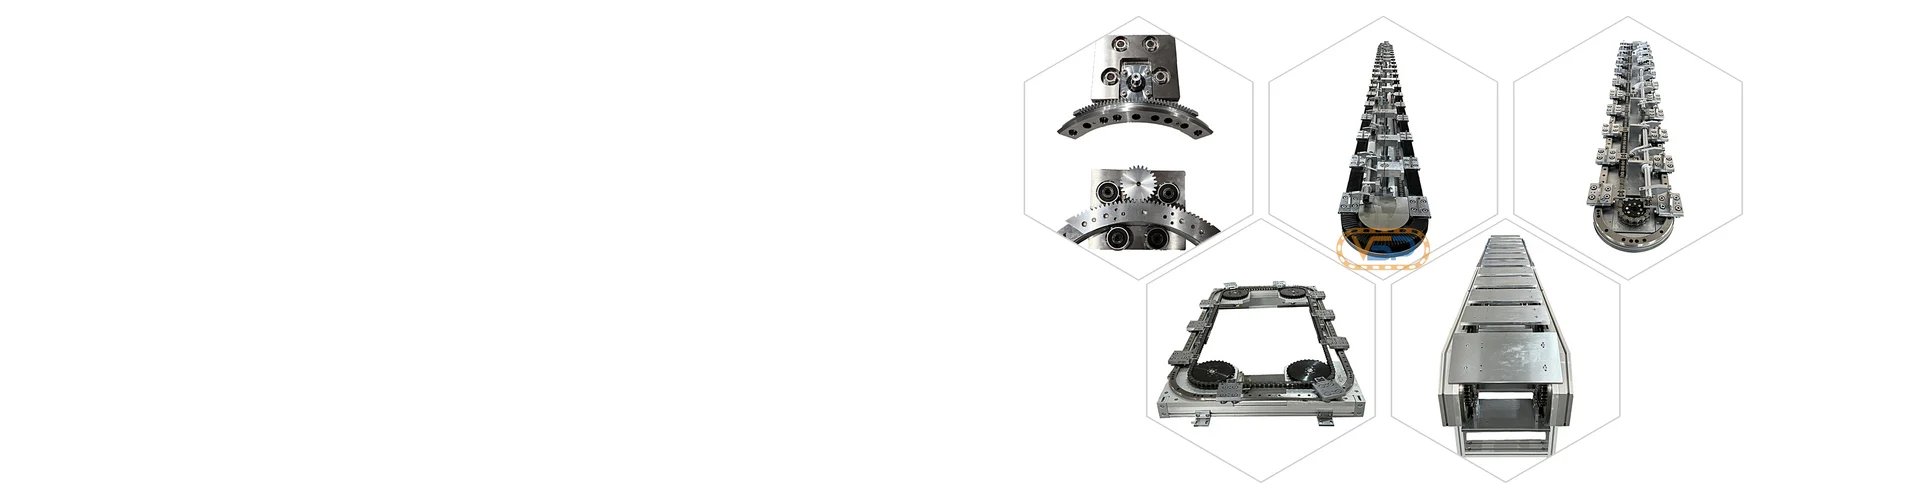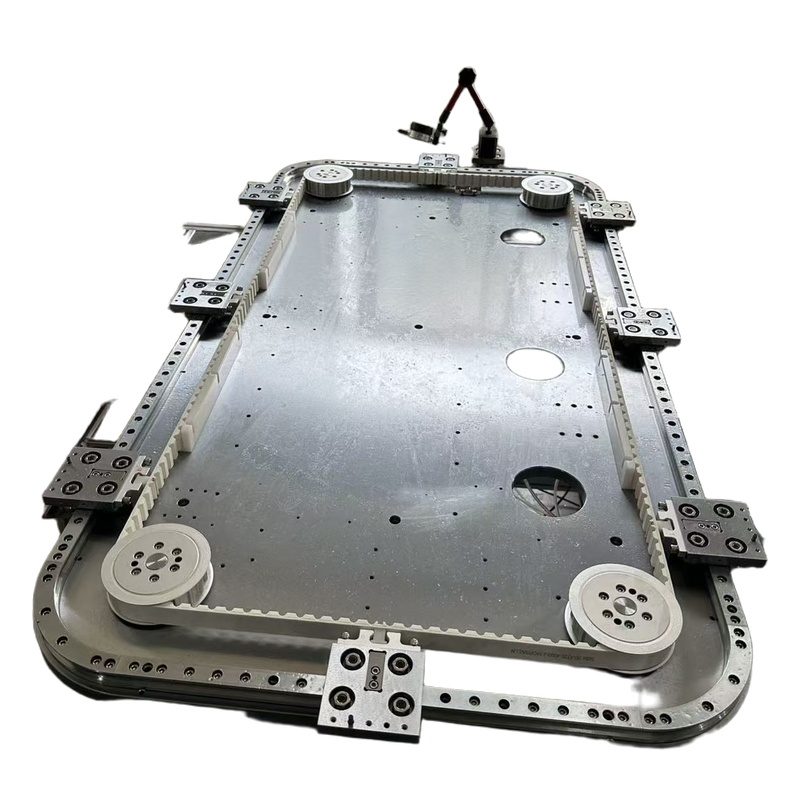
The starting point for ring guide rail selection is not the model, but the actual motion conditions. First list all the following parts on a single workstation: workpiece, jig, mounting plate, fixture, sensor bracket and possible cable drag chain. Judging solely by the weight of the workpiece will often underestimate the actual load.
The same total weight, but different center of gravity positions, have different effects on the carriages and arc segment. When the jig has a large overhang, an obvious eccentric load, there is impact when loading materials, or the load changes greatly between work stations, it is not advisable to only use the static weight for the initial selection. The maximum load, common load and possible eccentric load conditions should be provided together.
The chain type is usually used in situations where stable circulation and larger workstations are required; the belt or synchronous belt type is more suitable for medium-to-light load, low-noise or relatively clean processes; the cam linkage is suitable for fixed-cycle time indexing scenarios; the magnetic levitation solution needs to be comprehensively evaluated based on cleanliness requirements, carriers and control methods. No one drive method is better in all scenarios, the key is to match the load, movement pattern and tempo.
The arc segment is responsible for steering. The smaller the radius, the more compact the layout, but the working conditions of the carriages, fixture and load during cornering are also more severe. When selecting, you should first draw the maximum motion envelope of the arc guide rail outline, carriages, tooling and guard, and then determine whether the corresponding radius can be used.
The "center diameter" does not equal the actual footprint of the equipment. In addition to the guide rail itself, space must be reserved for fixture extension, splicing of adjacent straight sections, screw installation, sensors, cables and subsequent maintenance. For projects with tight space, it is recommended to use STEP or CAD models to complete assembly verification.
The equipment cycle time cannot be estimated only based on the theoretical uniform stroke. Acceleration, deceleration, indexing waiting, positioning confirmation and workstation movements will all take up time. The tighter the cycle time requirements, the more it is necessary to confirm the driving method, control strategy, vehicle quality and positioning method together.
Repeatable positioning accuracy is the deviation range of the slide when it returns to the same position multiple times, and is not equivalent to the final processing or assembly accuracy of the entire machine. Process allowable deviations, installation standards, fixture rigidity, drive control and inspection methods will all affect the final result.
A more effective way to ask questions is: where does the work station need to be positioned, what is the allowable deviation, what positioning method is used, and whether secondary positioning is needed. Only in this way can we judge how the guide rail, carriages, drive and clamp should cooperate.
If the project has clear requirements for repeated positioning, the installation base plate structure, datum plane, tooling weight and force direction should also be provided. If necessary, test items and acceptance criteria can be clarified during the plan confirmation stage to avoid looking at a single parameter and ignoring system conditions.
| Working condition characteristics | Priority content to check | Common misunderstandings |
|---|---|---|
| Multiple workstations, large load | Total mass, offset load, center of gravity, drive and installation structure | Only the workpiece weight is provided, ignoring the fixture and mounting plate |
| Compact space and small arc | Jig sweeps, arc profiles, maintenance and cable clearance | Only reserve equipment space according to the center diameter |
| The cycle time is tight | Acceleration and deceleration, positioning time, control method, vehicle quality | Calculate the cycle time directly according to the uniform stroke |
| There are positioning or detection requirements | Repeated positioning requirements, installation datums, fixtures and secondary positioning methods | Treat the single accuracy of the guide rail as the accuracy of the entire machine |
| Clean or low-noise scenes | Materials, lubrication restrictions, drive types, maintenance methods | Just look at the name without confirming the actual environment requirements |
If the equipment only reciprocates on a single axis and does not require multi-station closed-loop circulation or steering positioning, the linear guide solution may be more straightforward. The value of circular guide rails is mainly reflected in multi-station cyclic conveying, rotation positioning and closed-loop layout. First determine the production line action path, and then decide whether a ring structure is needed.
The essence of model selection is to check the load, arc radius, cycle time, accuracy and installation conditions in the same set of working conditions, and then confirm the specific model and drawings.

Precision conveying systems · Products and service
Products
Chain-driven ring guidesBelt-driven ring guidesPrecision link conveyorsCurved and linear guide componentsMagnetic levitation conveyorsCam-link ring guidesAbout us
Company profileOur facilitiesCertifications VideosApplicationsApplications
Automotive & new energy Precision electronics assembly Consumer electronicsMedical devicesNew energyPrecision dispensingNews
Company news Industry news NewsContact us
Contact details WhatsApp Business
Contact details+86 18912659251
Links: